Please take care when trading with people you don't know personally. To safeguard yourself as much as possible do/check the following:
- check the other party's ebay feedback (check his profile on TB, or ask for ebay ID) Send them an email through ebay to make sure.
- ask for references at this forum.
- check the members status on TB. Is this his first and only post or an experienced/well known member?
- Only pay through a secure payment provider, like Paypal. Make sure you pay for an item, not for a Service, as a Gift or other types of payment.
- Exchange real names and telephone numbers up front, and check them out.
- only offer shipping with full online tracking.
TamiyaBase.com is not a party in trades made on the basis of this site. Buyer and seller are sole responsible for their trades and for working out a safe way of payment and delivery.
- check the other party's ebay feedback (check his profile on TB, or ask for ebay ID) Send them an email through ebay to make sure.
- ask for references at this forum.
- check the members status on TB. Is this his first and only post or an experienced/well known member?
- Only pay through a secure payment provider, like Paypal. Make sure you pay for an item, not for a Service, as a Gift or other types of payment.
- Exchange real names and telephone numbers up front, and check them out.
- only offer shipping with full online tracking.
TamiyaBase.com is not a party in trades made on the basis of this site. Buyer and seller are sole responsible for their trades and for working out a safe way of payment and delivery.
TOPIC:
Ford Ranger front body mount 10 years 9 months ago #36626
|
|
Please Log in to join the conversation. |



 (saves you two hours
 )


Ford Ranger front body mount 10 years 9 months ago #36629
|
|
Please Log in to join the conversation. |

Ford Ranger front body mount 10 years 9 months ago #36631
|
|
Please Log in to join the conversation. |
Ford Ranger front body mount 10 years 9 months ago #36640
|
|
Please Log in to join the conversation. |
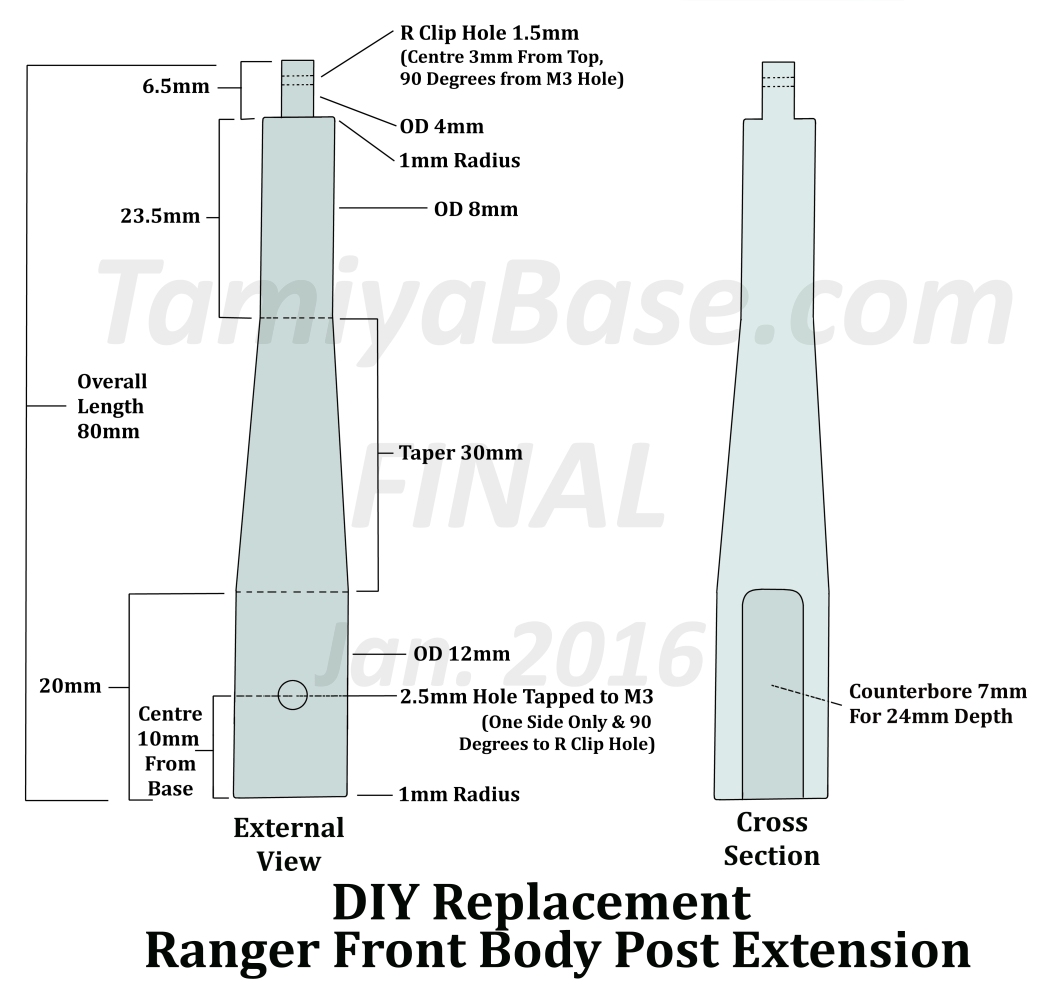

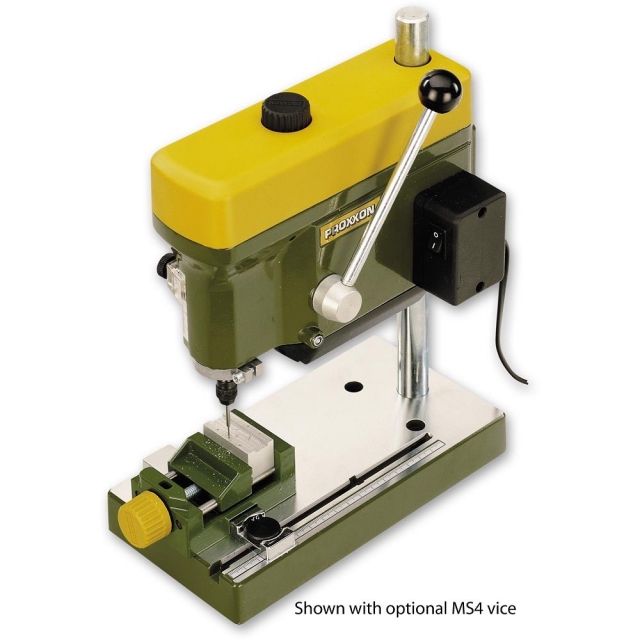

 or am i off on my scales think I even did .3mm last time on alloy (thats the rough bit final cut way less)
Ford Ranger front body mount 10 years 9 months ago #36645
|
|
Please Log in to join the conversation. |

Time to create page: 0.188 seconds
